Skip to content
ISTA Passed, Shelf Failed: Compression Specs for Retail-Ready Tissue Shippers
Short answer: an ISTA pass proves your carton survived a laboratory sequence measured in hours; it does not prove it will survive weeks of static stacking in a humid container. Retail-ready facial tissue shippers fail on shelves for three reasons the standard test under-weights: corrugated compression strength falls sharply as humidity rises, low-density products like folded tissue give the box almost no internal support, and perforated display openings remove board exactly where the load path runs. The fix is a written specification built on two numbers, not one: an edge crush test (ECT) value chosen for your humidity lane, and a finished-box compression (BCT) minimum measured after humidity conditioning, with rules that keep perforations and corners out of the load path.
Nothing erodes a facial tissue program faster than the telephone call from the distribution center: cartons that passed certification arrive with crushed corners, bowed front panels, and a reject rate that quietly climbs from one percent to eight as the pallet ages in a warm warehouse. The natural response, ordering thicker board, usually overpays for weight without fixing the failure, because the failure is not a board-strength deficit in dry conditions. It is a gap between what the certification test simulates and what an ocean container actually does to paper: sustained top load, cyclic condensation, and display features that weaken the very walls carrying the stack.
Why a Pass Certificate and an Eight Percent Reject Rate Coexist
Laboratory transit tests are compressions of time. A protocol that approximates drops, vibration and stacking runs its sequence in hours, and its compression element is applied briefly at a calculated load. A container voyage applies its stacking load for weeks, through day-night temperature swings that push humid air against fiber and pull it back, and through handling events that no distribution model fully predicts. Corrugated board loses a substantial share of its compression strength as relative humidity climbs, and the loss is not linear: a box that performs to specification at standard laboratory conditioning can fall far short of it in a container that sweats. The certificate is honest; the lane is simply harder than the certificate’s lane. The International Safe Transit Association, whose procedures underpin these certificates, maintains the official library of ISTA test procedures and is candid that procedure choice must match the distribution environment being simulated.
Tissue makes this worse than almost any other retail category. Canned goods and bottled products carry part of the stacking load internally; folded facial tissue does the opposite, behaving as a soft, compressible filler that offers the carton walls no reinforcement at all. Every vertical newton travels through the paperboard. When the retail-ready shipper also has a perforated display opening, the board removed for that opening tends to sit near the top and front of the panel, and corner creases that carry the load get scored to make the tear-away easier. The box is asked to be a warehouse load carrier and a retail fixture at once, and the two jobs disagree. For e-commerce shipments the same logic is codified in the ISTA-6 ship-in-own-container standard, which is worth reading alongside this article because it shows where the certification mindset helps and where it stops.
There is also a plain arithmetic issue: reject percentages concentrate at the bottom of the stack. If the bottom two layers of a pallet take the crush, the reported problem arrives as “eight percent of units,” while the engineering problem is “the bottom-layer box compression value is below what this lane demands.” Diagnosing by layer, before ordering thicker board, saves an entire iteration.
ECT and BCT: The Two Numbers That Belong in the Specification
Corrugated buyers habitually specify board by ECT, the edge crush test, which measures how much edgewise compression the board itself withstands. ECT is a good purchasing control because it is fast, cheap and tightly correlated with finished-box strength, but it is a board property, not a box property. The number that predicts whether your shipper survives the pallet is BCT, box compression strength: the force at which the actual finished carton, with its actual dimensions, creases, cutouts, glue joint and printing, fails in a compression frame. Two boxes made from identical board can differ meaningfully in BCT if one has a taller panel span, deeper scores, or a perforation across a corner. The specification that works names both: a minimum ECT for the board you will buy, and a minimum BCT for the finished shipper, with the BCT requirement calculated from your real pallet configuration rather than copied from a catalog. The corrugated industry’s own trade association, the Fibre Box Association, is the reference point most box plants use for these test methods and their interpretation.
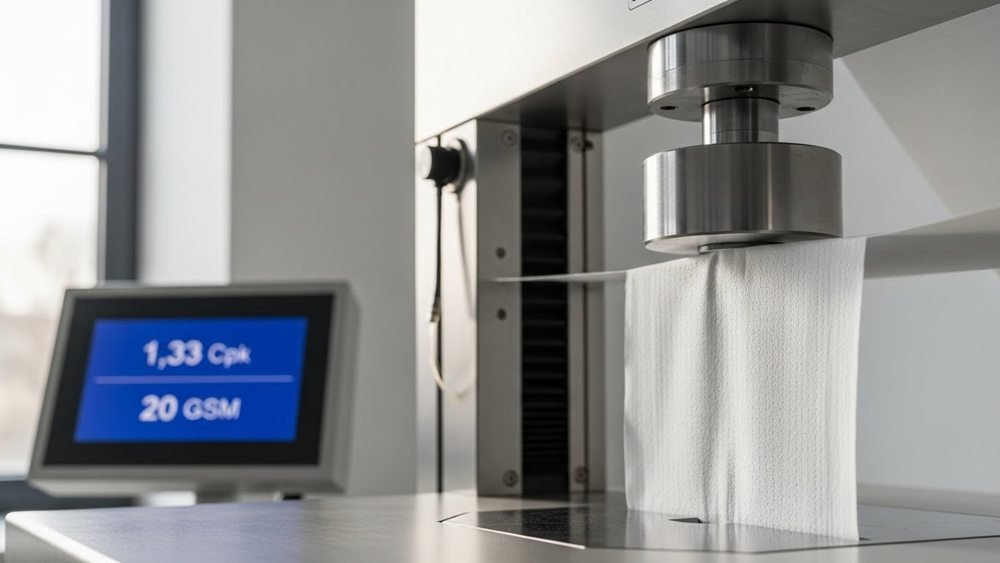
The humidity condition is what turns this from paperwork into prevention. Board conditioning before compression testing changes the result; testing the finished shipper after conditioning representative of your route, elevated humidity and elevated temperature, rather than only at standard atmosphere, is the difference between a number that predicts the voyage and one that predicts the laboratory. Ask suppliers to report both: ECT of the board by its standard method, and BCT of the finished, printed, die-cut carton after humidity conditioning. A supplier who volunteers both numbers and the methods behind them is telling you how they think; a supplier who can only quote a board grade is telling you something too.
Design Rules That Move the Failure Point
Board upgrades work, but geometry decides where the box fails, and four geometric rules carry most of the value. First, protect the corner columns. Vertical corners carry the stacking load in a corrugated box, so perforations, tear strips and deep scores must not cross them; a display opening should sit below the primary compression zone with a continuous structural beam above it, and the four corner columns should remain solid board from top to bottom. Second, manage panel span: taller, wider unsupported panels bow at lower loads, so internal fit matters. Tissue boxes packed with modest clearance, supported by partitions or a tight inner bundle, brace the outer walls instead of leaving them free to buckle. Third, close the load path through the pallet: footprints inside the pallet edge, zero overhang, column-stacked layers with corners aligned, and flat, rigid pallet decks. Overhang converts a corner from a column into a cantilever, and a few centimeters of it can remove a startling fraction of the stack’s effective strength. Fourth, match the flute architecture to the job: single-wall fine flutes for compact, light displays; double-wall constructions where stacking heights, humidity or handling intensity justify the weight and cost.
Moisture management supports the geometry rather than replacing it. Moisture-resistant liners and water-resistant adhesives slow the strength decay that humidity causes; container desiccants and pallet hoods reduce the condensation the board must endure; and keeping cartons off a container floor that can collect water prevents the localized saturation that turns the bottom layer into pulp. None of these replaces the BCT-after-conditioning number; they raise the odds that the number survives contact with the voyage. For the container-loading side of the same system, the choices between cartons and poly-bundles are compared in the site guide to palletizing bulk tissue for ocean freight, and the same zero-overhang discipline applies to retail-ready displays.
The Acceptance Test That Predicts the Shelf
One change in the test plan closes most of the gap between certificate and shelf: add a sustained-load compression check on humidity-conditioned shippers, at a load derived from your actual pallet stack. The arithmetic is straightforward and belongs in the specification: count the layers above the bottom carton, multiply by the weight of a loaded shipper, apply the static compression safety factor appropriate to storage duration and humidity, and require the conditioned BCT minimum to exceed that derived load with margin. For long ocean lanes the storage factor rises; for short domestic ones it falls. A box that clears this bar has demonstrated the property your reject rate is actually measuring. Suppliers who already publish their transit-damage prevention checklist for facial tissue will recognize the requirement; the difference is that here the numbers are contractual, not advisory.
Run the same logic on the display feature itself. Open the perforation on sample shippers after conditioning and before compression, the way a stock clerk would, then compress: the shipper must still meet its residual load requirement with the panel opened or scored, because real distribution includes units that are opened, leaned on, and re-stacked at the distribution center. If the perforation cannot survive that sequence, the opening moves, the beam above it thickens, or the corner columns widen; the test tells you which before the ocean does.
Pilot the specification, do not merely file it. Load a production pallet, wrap and ship it on the actual lane, and audit the bottom two layers on arrival against the same photographic standard used in pre-shipment inspection. One lane trial that arrives clean is worth more in negotiating power, internally and with the buyer, than a folder of certificates, because it demonstrates the whole system: board, geometry, palletizing and conditioning.
Writing It Into the Purchase Order
The clause that prevents the next eight percent is specific about numbers and silent about brand loyalty to any board grade. Specify: shipper board minimum ECT appropriate to the lane; finished, printed shipper minimum BCT after humidity conditioning representative of the route, calculated against the stated pallet configuration and storage duration; no perforation or score crossing a vertical corner column; display opening below the primary compression zone with a continuous structural header; internal fit that braces panels without crushing product; zero pallet overhang, column stacking and aligned corners documented with loading photographs; and retention of compression test reports by lot. Require the supplier to state the test methods for ECT and BCT and to identify who ran them.
This is also the clause that keeps a packaging conversation honest when a rejection does occur. With both numbers on file, the post-mortem compares the failing carton’s measured BCT against the specification and asks which condition drifted: board, geometry, palletizing or storage. Suppliers respond to that question with engineering, because it has an engineering answer, and the next shipment arrives with the fix rather than with thicker, heavier, more expensive board and the same reject rate.
Frequently Asked Questions
Does a higher ECT rating alone fix corner crush on facial tissue shippers?
No. ECT measures the board, while corner failures usually trace to geometry and humidity: perforations across load-bearing corners, unsupported panel spans, pallet overhang, and compression strength lost to moisture. Specify finished-carton BCT after humidity conditioning alongside a sensible ECT minimum, and enforce the geometric rules in the die-line.
Why did our certified packaging still fail on the shelf?
Certification tests compress weeks of stacking and condensation into hours, so a pass confirms impact and vibration performance more than long-duration, high-humidity compression. Adding a sustained-load compression check on conditioned shippers, derived from your real pallet stack, closes the gap.
What single number should we agree with the supplier first?
The finished-shipper BCT minimum after humidity conditioning, calculated from your pallet configuration. ECT stays in the specification as a board purchasing control, but the BCT number is the one that predicts whether the bottom layers survive the lane.